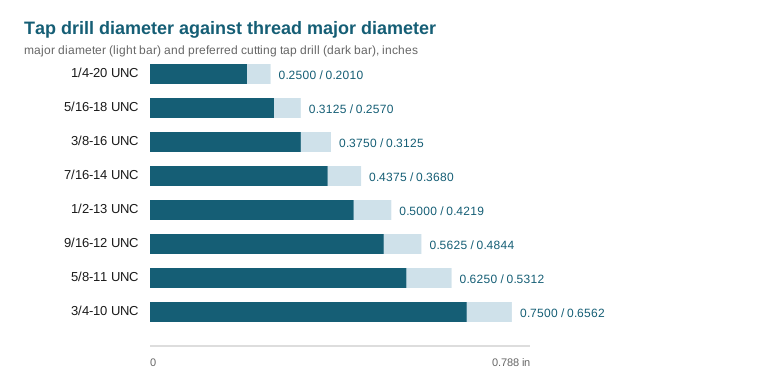
The preferred cutting tap drill for every unified thread we have verified, coarse and fine, from #0 to 4 inch, with the drill size in inches and millimetres.
Designations follow the standard form: nominal size, threads per inch, then the series. Where a drill is marked as approximate in the source table it is left out rather than rounded.
| Thread | Major dia (in) | Major dia (mm) | TPI | Tap drill | Drill dia (in) | Drill dia (mm) |
|---|---|---|---|---|---|---|
| #0-80 UNF | 0.0600 | 1.524 | 80 | 3/64 | 0.0469 | 1.191 |
| #1-64 UNC | 0.0730 | 1.854 | 64 | #53 | 0.0595 | 1.511 |
| #1-72 UNF | 0.0730 | 1.854 | 72 | #53 | 0.0595 | 1.511 |
| #2-56 UNC | 0.0860 | 2.184 | 56 | #50 | 0.0700 | 1.778 |
| #2-64 UNF | 0.0860 | 2.184 | 64 | #50 | 0.0700 | 1.778 |
| #3-48 UNC | 0.0990 | 2.515 | 48 | #47 | 0.0785 | 1.994 |
| #3-56 UNF | 0.0990 | 2.515 | 56 | #45 | 0.0820 | 2.083 |
| #4-40 UNC | 0.1120 | 2.845 | 40 | #43 | 0.0890 | 2.261 |
| #4-48 UNF | 0.1120 | 2.845 | 48 | #42 | 0.0935 | 2.375 |
| #5-40 UNC | 0.1250 | 3.175 | 40 | #38 | 0.1015 | 2.578 |
| #5-44 UNF | 0.1250 | 3.175 | 44 | #37 | 0.1040 | 2.642 |
| #6-32 UNC | 0.1380 | 3.505 | 32 | #36 | 0.1065 | 2.705 |
| #6-40 UNF | 0.1380 | 3.505 | 40 | #33 | 0.1130 | 2.870 |
| #8-32 UNC | 0.1640 | 4.166 | 32 | #29 | 0.1360 | 3.454 |
| #8-36 UNF | 0.1640 | 4.166 | 36 | #29 | 0.1360 | 3.454 |
| #10-24 UNC | 0.1900 | 4.826 | 24 | #25 | 0.1495 | 3.797 |
| #10-32 UNF | 0.1900 | 4.826 | 32 | #21 | 0.1590 | 4.039 |
| #12-24 UNC | 0.2160 | 5.486 | 24 | #16 | 0.1770 | 4.496 |
| #12-28 UNF | 0.2160 | 5.486 | 28 | #14 | 0.1820 | 4.623 |
| #12-32 UNEF | 0.2160 | 5.486 | 32 | 3/16 | 0.1875 | 4.763 |
| 1/4-20 UNC | 0.2500 | 6.350 | 20 | #7 | 0.2010 | 5.105 |
| 1/4-28 UNF | 0.2500 | 6.350 | 28 | #3 | 0.2130 | 5.410 |
| 1/4-32 UNEF | 0.2500 | 6.350 | 32 | 7/32 | 0.2188 | 5.556 |
| 5/16-18 UNC | 0.3125 | 7.938 | 18 | F | 0.2570 | 6.528 |
| 5/16-24 UNF | 0.3125 | 7.938 | 24 | I | 0.2720 | 6.909 |
| 5/16-32 UNEF | 0.3125 | 7.938 | 32 | 9/32 | 0.2812 | 7.144 |
| 3/8-16 UNC | 0.3750 | 9.525 | 16 | 5/16 | 0.3125 | 7.938 |
| 3/8-24 UNF | 0.3750 | 9.525 | 24 | Q | 0.3320 | 8.433 |
| 3/8-32 UNEF | 0.3750 | 9.525 | 32 | 11/32 | 0.3438 | 8.731 |
| 7/16-14 UNC | 0.4375 | 11.113 | 14 | U | 0.3680 | 9.347 |
| 7/16-20 UNF | 0.4375 | 11.113 | 20 | 25/64 | 0.3906 | 9.922 |
| 7/16-28 UNEF | 0.4375 | 11.113 | 28 | Y | 0.4040 | 10.262 |
| 1/2-13 UNC | 0.5000 | 12.700 | 13 | 27/64 | 0.4219 | 10.716 |
| 1/2-20 UNF | 0.5000 | 12.700 | 20 | 29/64 | 0.4531 | 11.509 |
| 1/2-28 UNEF | 0.5000 | 12.700 | 28 | 15/32 | 0.4688 | 11.906 |
| 9/16-12 UNC | 0.5625 | 14.287 | 12 | 31/64 | 0.4844 | 12.303 |
| 9/16-18 UNF | 0.5625 | 14.287 | 18 | 1/2 | 0.5000 | 12.700 |
| 9/16-24 UNEF | 0.5625 | 14.287 | 24 | 33/64 | 0.5156 | 13.097 |
| 5/8-11 UNC | 0.6250 | 15.875 | 11 | 17/32 | 0.5312 | 13.494 |
| 5/8-18 UNF | 0.6250 | 15.875 | 18 | 9/16 | 0.5625 | 14.287 |
| 5/8-24 UNEF | 0.6250 | 15.875 | 24 | 37/64 | 0.5781 | 14.684 |
| 3/4-10 UNC | 0.7500 | 19.050 | 10 | 21/32 | 0.6562 | 16.669 |
| 3/4-16 UNF | 0.7500 | 19.050 | 16 | 11/16 | 0.6875 | 17.462 |
| 3/4-20 UNEF | 0.7500 | 19.050 | 20 | 45/64 | 0.7031 | 17.859 |
| 7/8-9 UNC | 0.8750 | 22.225 | 9 | 49/64 | 0.7656 | 19.447 |
| 7/8-14 UNF | 0.8750 | 22.225 | 14 | 51/64 | 0.7969 | 20.241 |
| 7/8-20 UNEF | 0.8750 | 22.225 | 20 | 53/64 | 0.8281 | 21.034 |
| 1-8 UNC | 1.0000 | 25.400 | 8 | 7/8 | 0.8750 | 22.225 |
| 1-12 UNF | 1.0000 | 25.400 | 12 | 59/64 | 0.9219 | 23.416 |
| 1-20 UNEF | 1.0000 | 25.400 | 20 | 61/64 | 0.9531 | 24.209 |
The usual shop rule is major diameter minus one thread pitch, where the pitch is one divided by the threads per inch. That gives roughly 75 percent thread engagement, which is the point where the thread is strong enough while the tap still cuts freely. The table above takes the nearest standard drill at or below that value rather than the exact arithmetic, because the drill has to be a size you can actually buy.
A #21 drill, 0.1590 in (4.039 mm). A 10-32 UNF thread has a major diameter of 0.1900 in and 32 threads per inch.
A #7 drill, 0.2010 in (5.105 mm). The quick rule is major diameter minus one thread pitch, which gives 0.2000 in; the nearest standard drill below that is #7.
A 5/16 drill, 0.3125 in (7.938 mm).
Tapping does not remove the full thread depth; the drill sets the minor diameter and the tap cuts the flanks. A hole at major diameter would leave no material for the threads to cut, while a hole that is too small overloads the tap and risks breakage.
No. A finer thread has more threads per inch, so its pitch is smaller and its tap drill is larger. The table gives a separate drill for each series.